
Steel Defects Seams on Rolled Steel Products
Learn how to detect and avoid defect seams in rolled steel products.


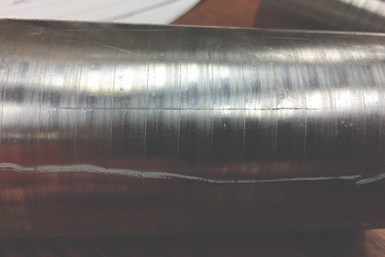
Most defects in steel workpieces encountered in our precision machine shops are longitudinal in nature. This means that they go lengthwise with the bar, not transversely across the bar.
“Seams are longitudinal crevices that are tight or even closed at the surface, but are not welded shut. They are close to radial in orientation and can originate in steelmaking, primary rolling or on the bar or rod mill.”– AISI Technical Committee on Rod and Bar Mills, Detection, Classification, and Elimination of Rod and Bar Surface Defects


Seams are straight and can vary in length — often running the length of several bars — due to elongation of the product (and the initiating imperfection) during bar rolling.
Seams may be present in the billet before bar rolling as a result of non-metallic inclusions, cracking, tears, subsurface cracking or porosity. During continuous casting, loss of mold level control can result in out-of-control conditions which can reseal while in the mold but leave a weakened surface. Seam frequency is higher in resulfurized steels compared to non-resulfurized grades. Seams are generally less frequent in fully deoxidized steels.
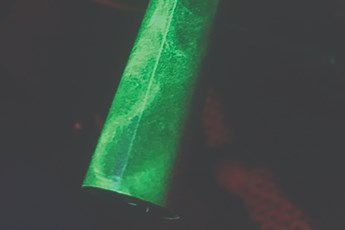
In our shops, seams can be detected visually by eye and magnaglo magnetic particle methods. Another method to confirm the presence of seams in our barstock is an upset test, which compresses a short piece of the steel to expand its diameter — it will split longitudinally where a seam is present. Bending a bar can reveal the presence of surface defects such as seams; they can open up as the material is bent.
Another way to confirm the presence of a seam is to file the bar to make a flat until the dark indication just disappears. A micrometer reading of the depth where the indication disappears subtracted from the bar’s original diameter results in a measurement of the seam’s depth. So, on a steel sample, if it has a straight, longitudinal, linear indication that when file down shows a dark line against the brighter base metal, it is a seam.
“These long, straight, tight, linear defects are the result of gasses or bubbles formed when the steel solidified. Rolling causes these to lengthen as the steel is lengthened. Seams are dark, closed, but not welded”- Miles Free III’s 1986 Junior Metallurgist definition taken from his lab notebook.
Rejection criteria are subject to negotiation with your supplier — as are detection limits for various inspection methods. Because seams can occur anywhere on a rolled product, stock removal allowance is applied on a per side basis.
If the stock must absolutely be seam free, order turned and polished or cold drawn, turned and polished material. The stock removal assures that the seamy outer material has been removed.
ASTM A108 Table A1.8 Surface Discontinuity Tolerances for Cold-Finished Steel Bar provides both Maximum Allowable Surface Discontinuity Depth (what you find when you file down until the indication disappears) and the recommended Stock Removal Depth per Side of Bar.
Note that resulfurized materials are more prone to surface imperfections, so tolerances and stock removal requirements are increased accordingly.


Related Content

The Workforce Challenge and Why Traditional Hiring Isn’t Enough, Part 1
The workforce shortage is a business risk, not just a human resources problem.
Read More
Craftsman Cribsheet No. 134: ISO Material Groups: Steel
How to interpret the machinability of various forms of steel.
Read More
Craftsman Cribsheet No. 133: Identifying ISO Workpiece Material Groups
When selecting the right tooling for a job, it is important to understand how that selection will impact your end results.
Read More
The Lost Art of Mastery
There is value to honing and mastering a craft. But it takes time and experience.
Read MoreRead Next

Finding the Right Tools for a Turning Shop
Xcelicut is a startup shop that has grown thanks to the right machines, cutting tools, grants and other resources.
Read More
WEBINAR: From Machine Data to Guided Action: How Modern Shops Are Closing the Execution Gap
In this webinar, MachineMetrics Product Manager Josh Fish is joined by Pindel Global Precision's Thomas Deslongchamps, for a candid look at what closing the execution gap actually looks like inside a precision machining shop.
Read More
Webinar Recap: Streamlining Swiss Machining Through Automation
See how CAMWorks 2026 cuts Swiss-style CNC programming time by 70%+ with automatic feature recognition, full machine simulation, and smart segmentation tools.
Read More


